African Boatbuilding Runs at Two Different Rhythms
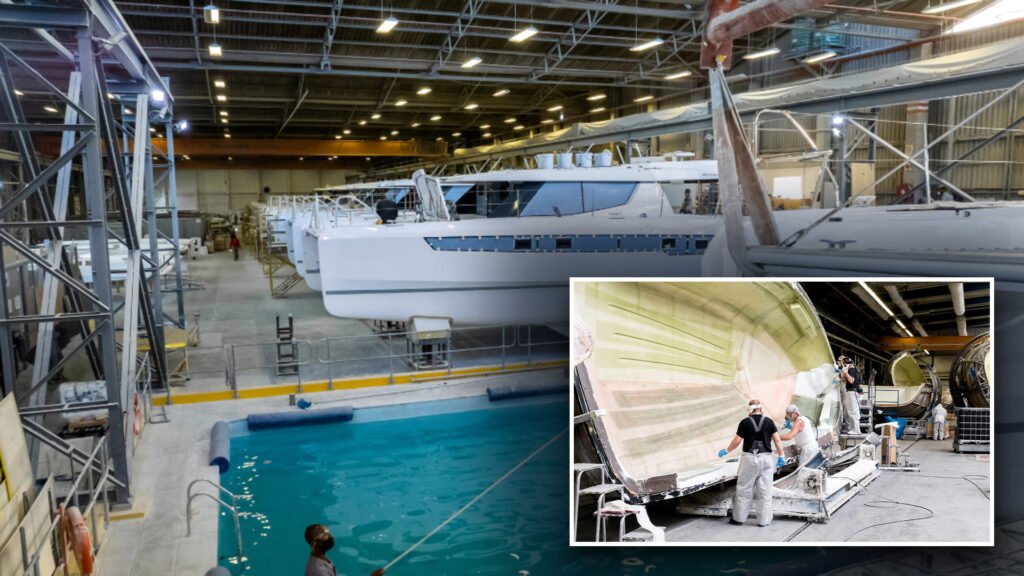
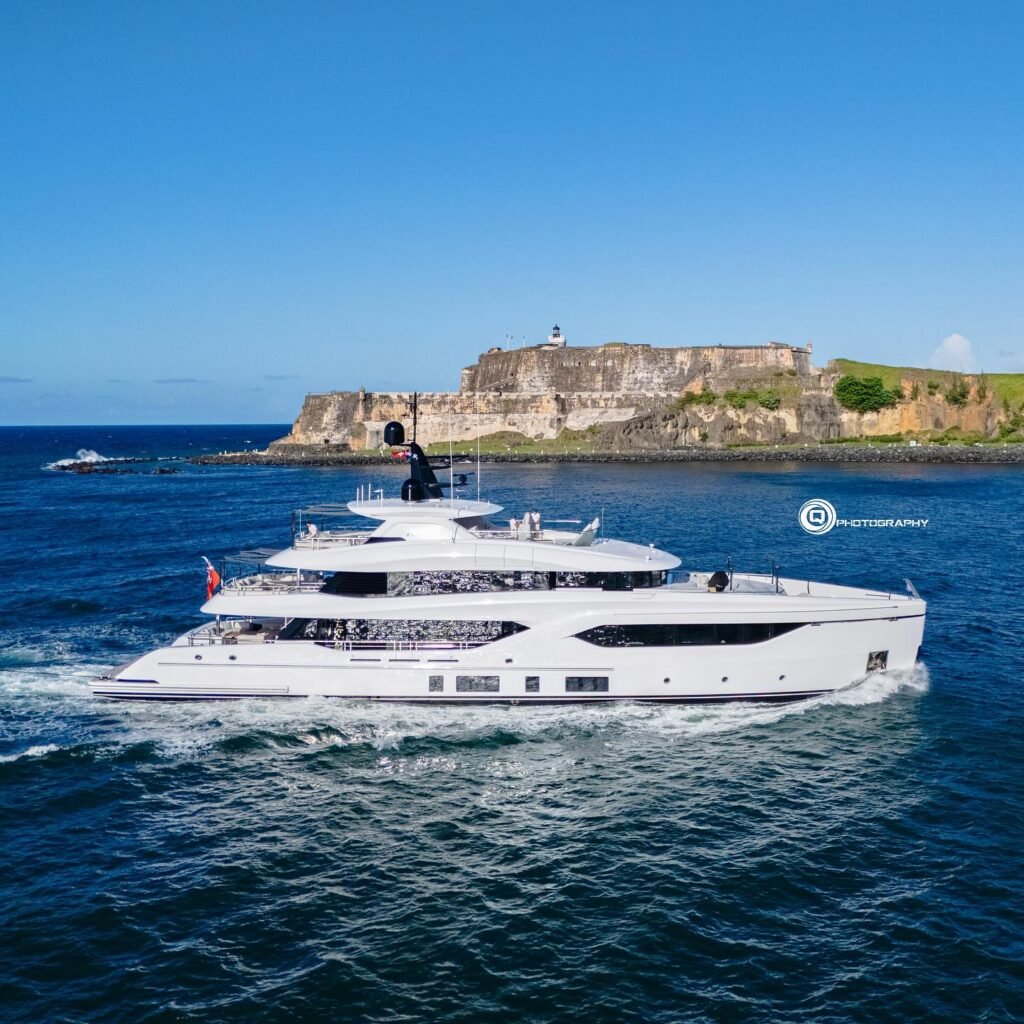
Cape Town, Knysna and Durban host the continent’s largest cluster of FRP boatbuilders: catamarans and motor yachts built in series, largely for export to Europe and North America. East and West Africa run at a different rhythm — Tanzania (including Zanzibar), Kenya, Mozambique, Nigeria, Ghana and Senegal are dominated by smaller yards working in hand lay-up, building fishing boats, passenger ferries and patrol craft, and taking on hull repairs. Renewal programmes for fishing fleets in East Africa have added a further stream of new-build work in the past two years.
Batch size and process discipline differ between the two, but the working environment is much the same: tropical or subtropical coast, high temperature, high humidity, salt air, and workshops that are rarely temperature or humidity controlled. And the layer that decides how long a hull lasts is the same in both: the chopped strand mat directly behind the gelcoat.
A hull starts at the mould: gelcoat, first mat layer, alternating chopped strand mat and woven roving, then structural stiffening. The chopped strand mat builds thickness, ties the plies together and separates the gelcoat from the load-bearing laminate. How well it goes down decides whether the hull carries voids, whether water finds a way in, and whether blisters appear a few years later.
Three Problems African Yards Meet Again and Again
Curved, Vertical and Overhead Surfaces: Once the Mat Bridges, There Is a Void Behind It
A hull is a double-curved surface. The topsides are vertical, the bottom and the keel transition are close to overhead, and the mat has to be pressed flat in all of them. Where it does not conform, it bridges at the bow knuckle, the sheer and the keel transition — the surface looks fair, but the mat has lifted off the mould. There is no resin in that void, and once the hull is in the water, water goes in there.
Moisture in a Humid Climate Becomes Voids Inside the Laminate
Workshop humidity on the tropical coast stays high year round. Mat is a porous material and takes up moisture from the air once the roll is opened. Mat with elevated moisture carries that water into the resin; during the exotherm of cure the water vaporises and leaves voids and micropores in the laminate. Those micropores are paths for water: after a few years in warm water, water molecules migrate into the resin, collect in the micropores and swell them, and blisters appear at the surface — osmosis.
Hand Lay-Up Depends on Feel, and Slow-Wetting Material Leaves Defects in the Hull
Most African yards laminate by hand, so quality depends on the operator. If resin penetrates slowly, the operator starts rolling the next ply before wet-out is complete, and white strands and dry patches are sealed between plies. The first layer shows it most clearly: a dry patch behind the gelcoat prints the woven roving pattern through to the surface, and in bad cases fine cracks follow. This is not necessarily inexperience — it is material that offers no tolerance for the pace of hand work.
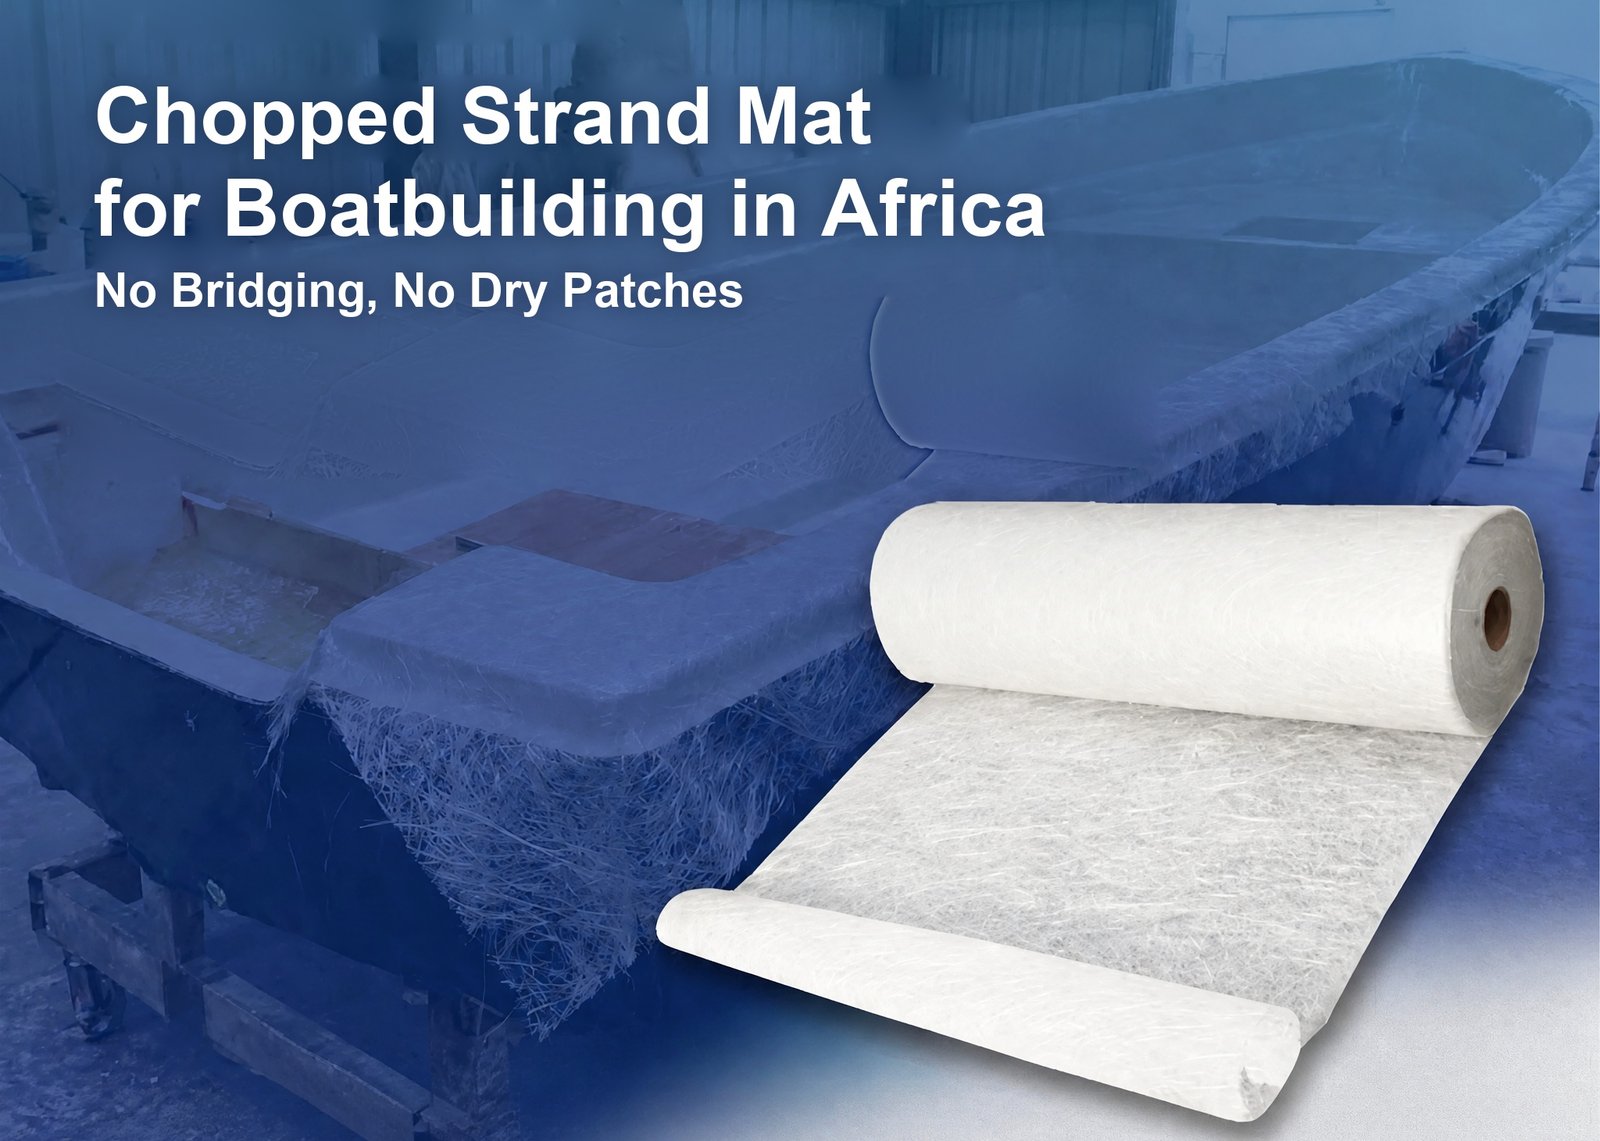
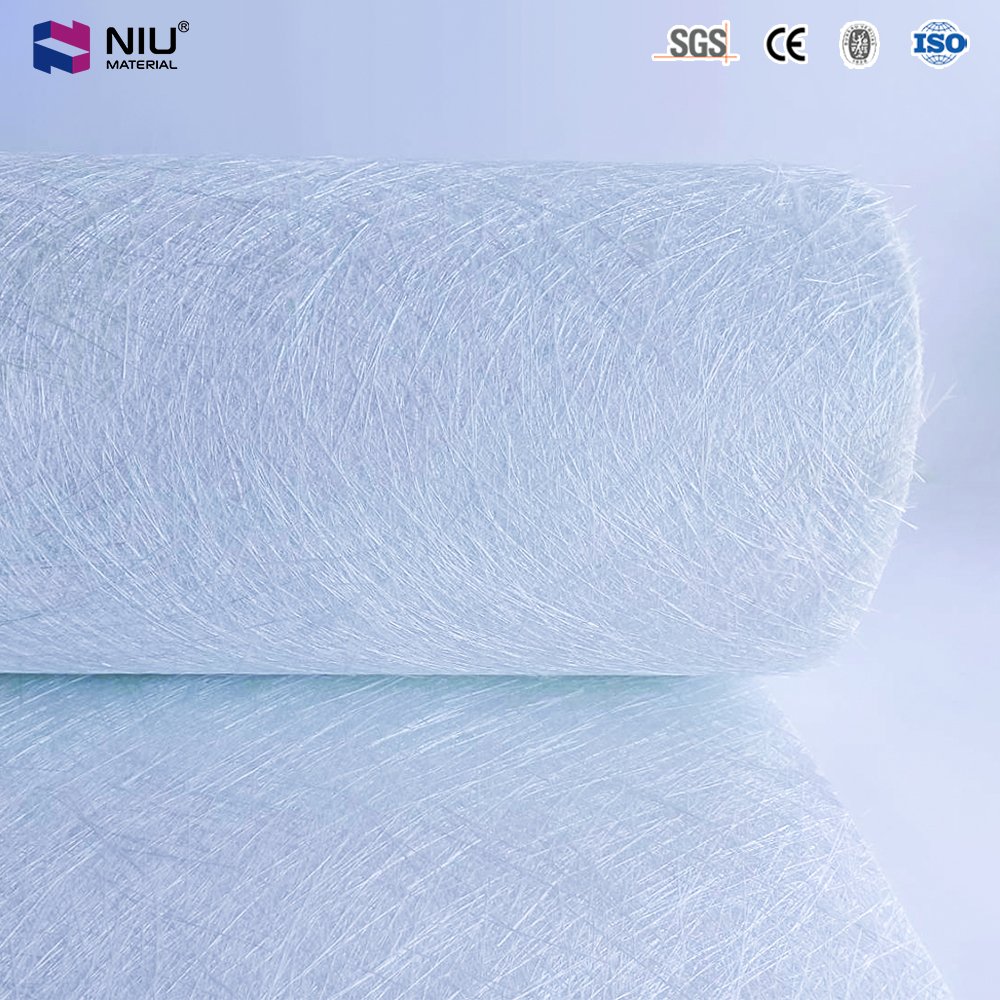
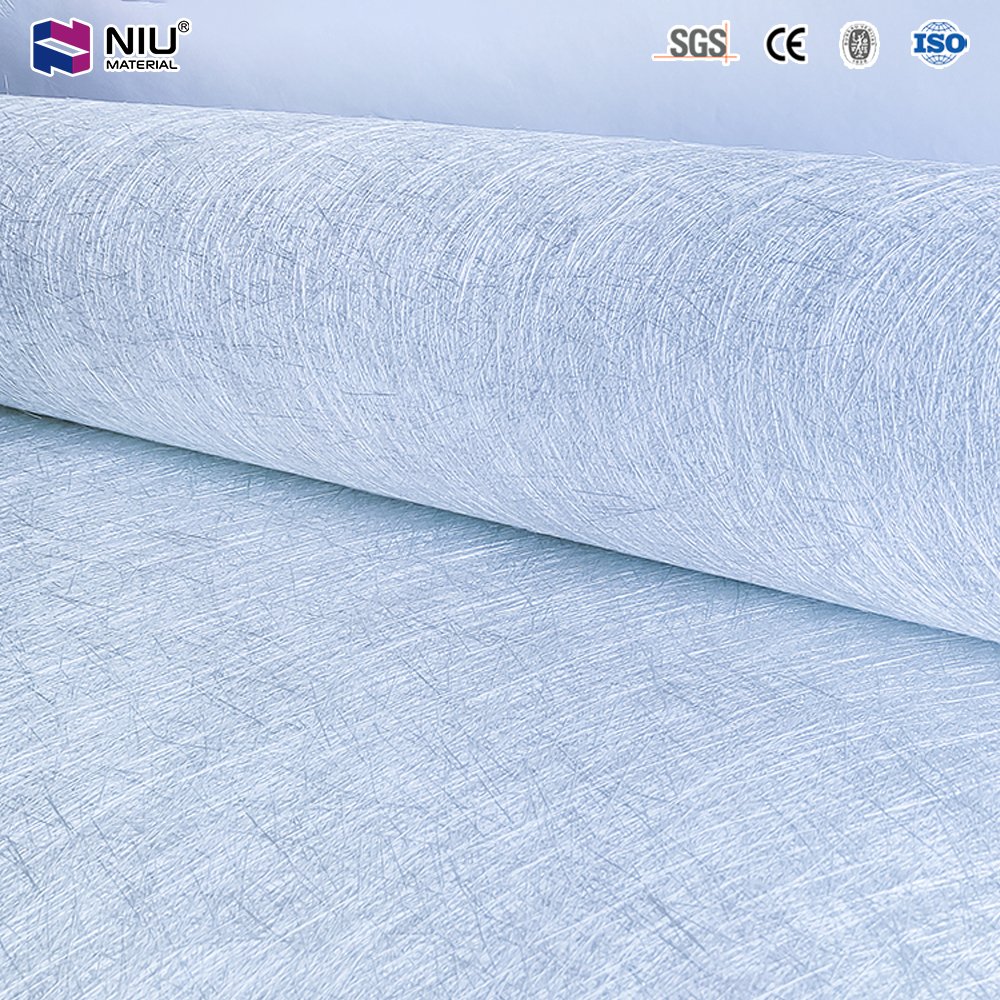
450 g/m² Chopped Strand Mat: Conformity, Wet-Out, Moisture Control
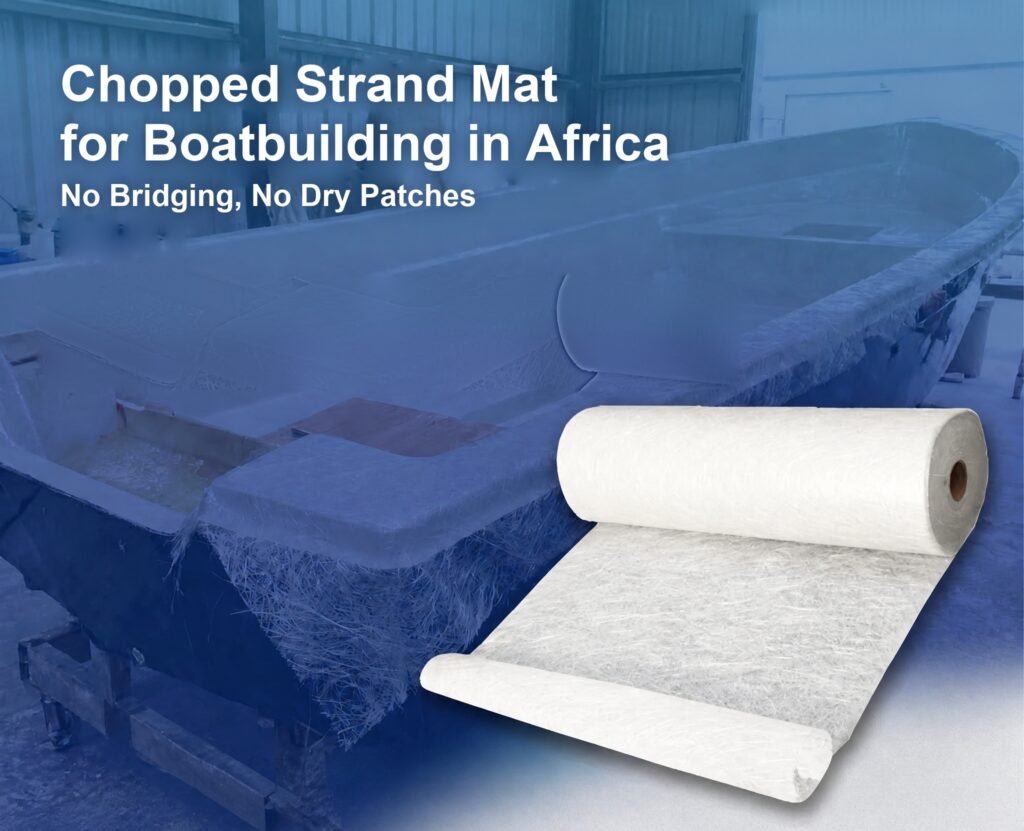
Our boatbuilding mat is 450 g/m² E-glass chopped strand mat, 1.27 m wide, powder-bonded. The weight sets thickness per ply and conformity; the width sets how many overlaps a hull carries along its length; the bonding method sets wet-out speed and the tolerance hand lay-up needs.
It Follows a Double Curvature, Without Bridging at Corners or Topsides
The fibres in chopped strand mat form a random web with no direction. Laid onto a double curvature, the material has slack in every direction and follows the shape, instead of springing back and arching the way a woven fabric does. At 450 g/m² there is enough substance for thickness while conformity is retained, so the mat can be pressed down onto the mould at the bow knuckle, the sheer and the keel transition.
When it sits down properly, there is no void between mat and mould, resin fills the space, and the surface is dense. For a hand lay-up yard this is the most direct gain: with the same operators and the same rolling time, there are far fewer bridged areas.
Powder Bonding Means Fast Penetration and Tolerance for Hand Work
The powder binder dissolves on contact with resin and forms no barrier ahead of the fibres, so resin travels from the face of the mat through to the back in one pass. Wet-out time is short: an operator laying the first ply over gelcoat does not have to wait, and air escapes more readily under the roller.
With the first ply fully wet out, the back of the gelcoat stays flat, the woven roving pattern is less likely to print through, and the risk of fine cracks falls. The same holds between plies: fewer white strands and dry patches, and the plies bond within one body of resin rather than being separated by dry fibre.
Controlled Moisture Keeps Storage and Cure Stable in the Tropics
Moisture content at despatch is held below 0.2%, and rolls are packed with a moisture barrier. African shipments travel by sea and are then stored in coastal warehouses where humidity is high and dwell time is long; if the packing is not sealed, the mat has already taken up moisture before the roll is opened.
Mat at low moisture carries no water into the resin, so cure leaves no vapour voids or micropores. A dense laminate gives water no path in, and there is one less starting point for osmotic blistering.
All Three Materials in the Hull Can Be Supplied Together
An FRP boat uses more than one glass fibre material, working outward from the mould face: surface mat for a dense first layer, chopped strand mat to build thickness and tie the plies, woven roving for the overall strength of the hull. If the three come from different plants their surface treatments differ and wet-out speeds do not match — the usual mismatch being surface mat that wets out quickly and chopped strand mat that lags behind, leaving an under-wetted interface between the first layer and the structural laminate.
We produce all three on one surface treatment formula: surface mat for the first layer, chopped strand mat for thickness and interlaminar connection, woven roving for load carrying. Used together they wet out and cure at the same pace, and changing material does not mean re-establishing the process.


About Us
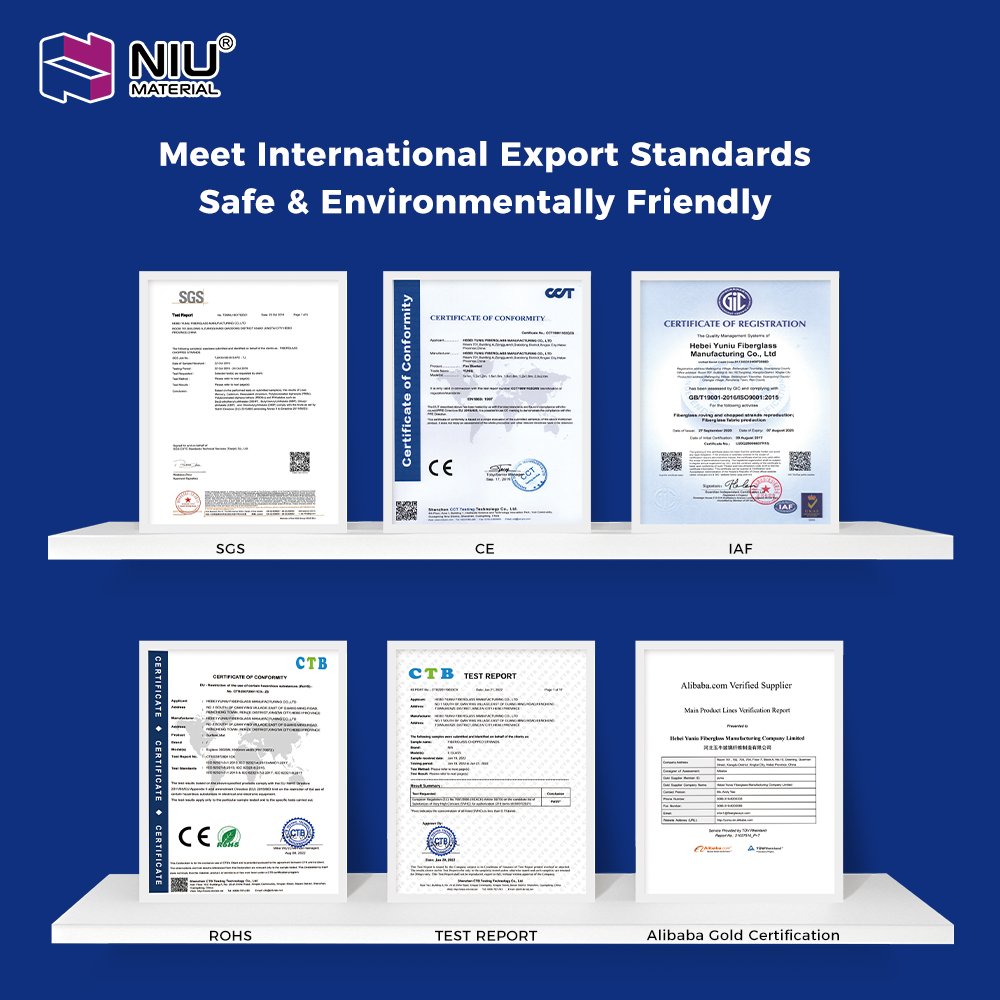
Hebei Yuniu Glass Fibre Manufacturing Co., Ltd. — brand Niumaterial / NIU® MATERIAL — was founded in 2012 in Hebei, China, and is a specialist glass fibre manufacturer in northern China with three R&D and production lines. The team brings more than twenty years of experience in the industry, products are exported to 128 countries and regions, and the company holds SGS, CE and ISO9001 certification.
Niumaterial’s quality control runs through the entire process from fibre drawing to finished packing, with weight, width, moisture and binder content tested batch by batch and reported. If moisture or weight drifts, voids and hull thickness drift with it, so both properties are controlled by batch.
Niumaterial’s chopped strand mat can be customised to your process: weight, width, roll length and packing format are all adjustable, with different specifications for hand lay-up and spray-up. On the export side, shipping plans are laid out by week, documents are issued consistently from the same entity, and long-cycle projects are followed up by email.
In Conclusion
African FRP boatbuilding runs from export-oriented series production at one end to small coastal yards and fleet renewal at the other, and requirements are rising on both: hulls lighter and thinner, in a service environment of heat, humidity and salt water. A hull’s life depends on how dense the laminate is, and that starts with the first layer of material.
Our 450 g/m² E-glass chopped strand mat, 1.27 m wide and powder-bonded, corresponds to the three most common problems in hull laminating: voids left by bridging over curvature, dry patches and print-through from incomplete wet-out, and water ingress through micropores in a hot, humid climate.
If you are an FRP boatbuilder, hull repair yard or glass fibre distributor in Africa, contact us for samples and technical datasheets, or to discuss a custom weight and width against your hull type, process and laminate schedule.